A carton transfer axis synchronized to the conveyor
Design the pusher around the product window, not an isolated actuator speed rating.
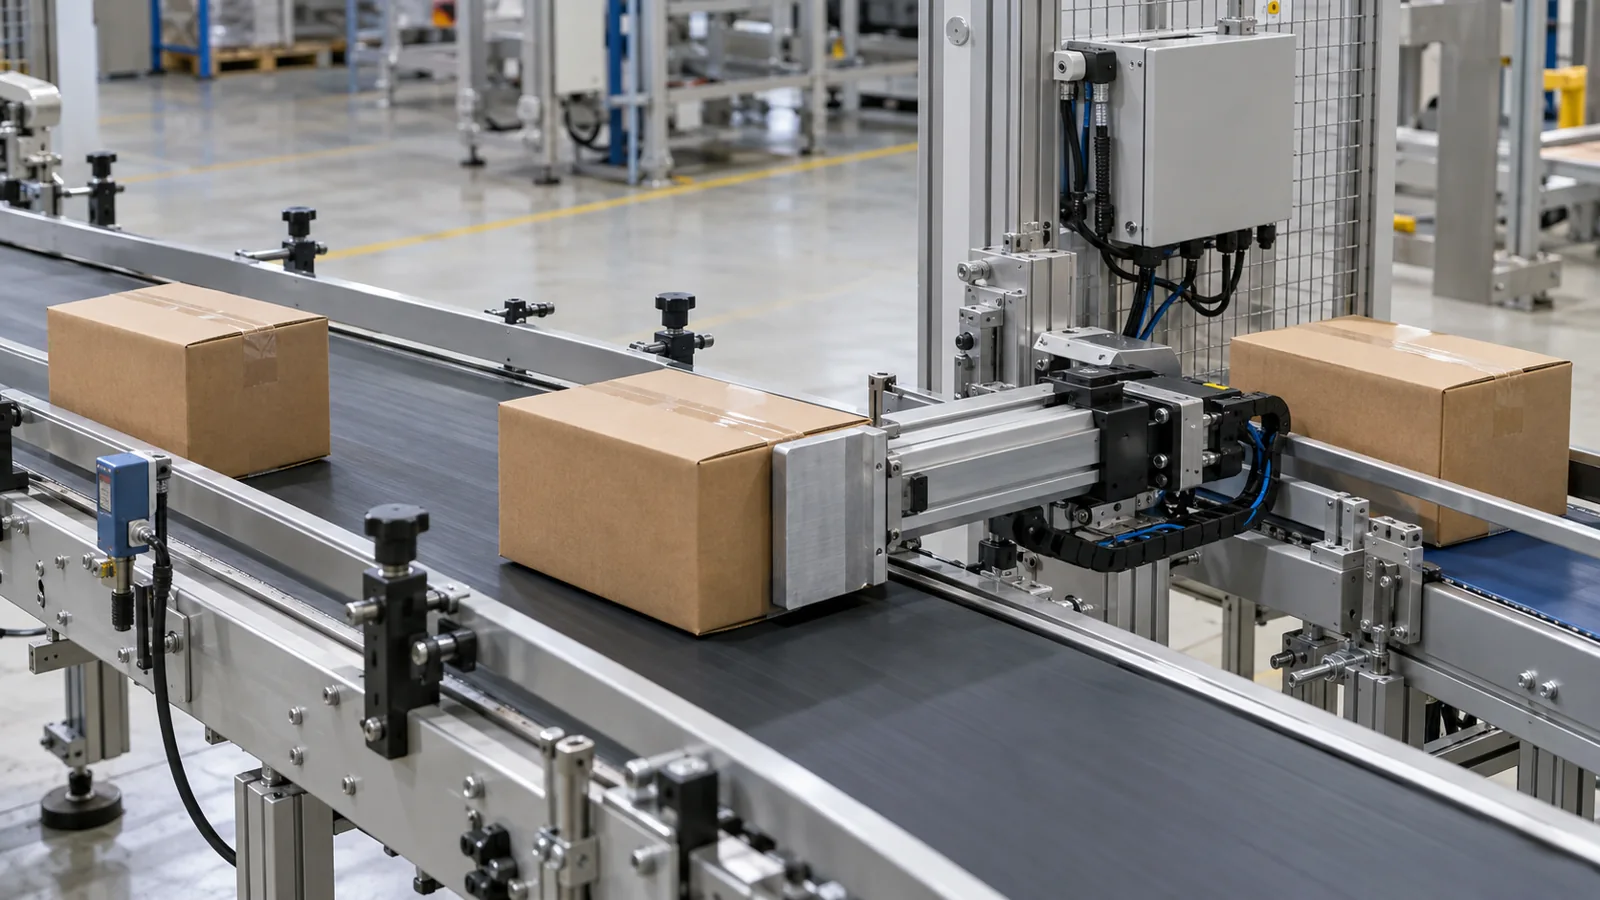
What this axis must achieve.
Product / operation
Carton sorting and lane transfer
Engineering example
20 kg carton; 300 mm transfer travel
Motion example
0.6 m/s peak pusher velocity; 2 m/s² acceleration
Engineering feasibility study: assumed inputs and calculated values; conceptual equipment illustrations. Proposed checks require project approval and measured trials.
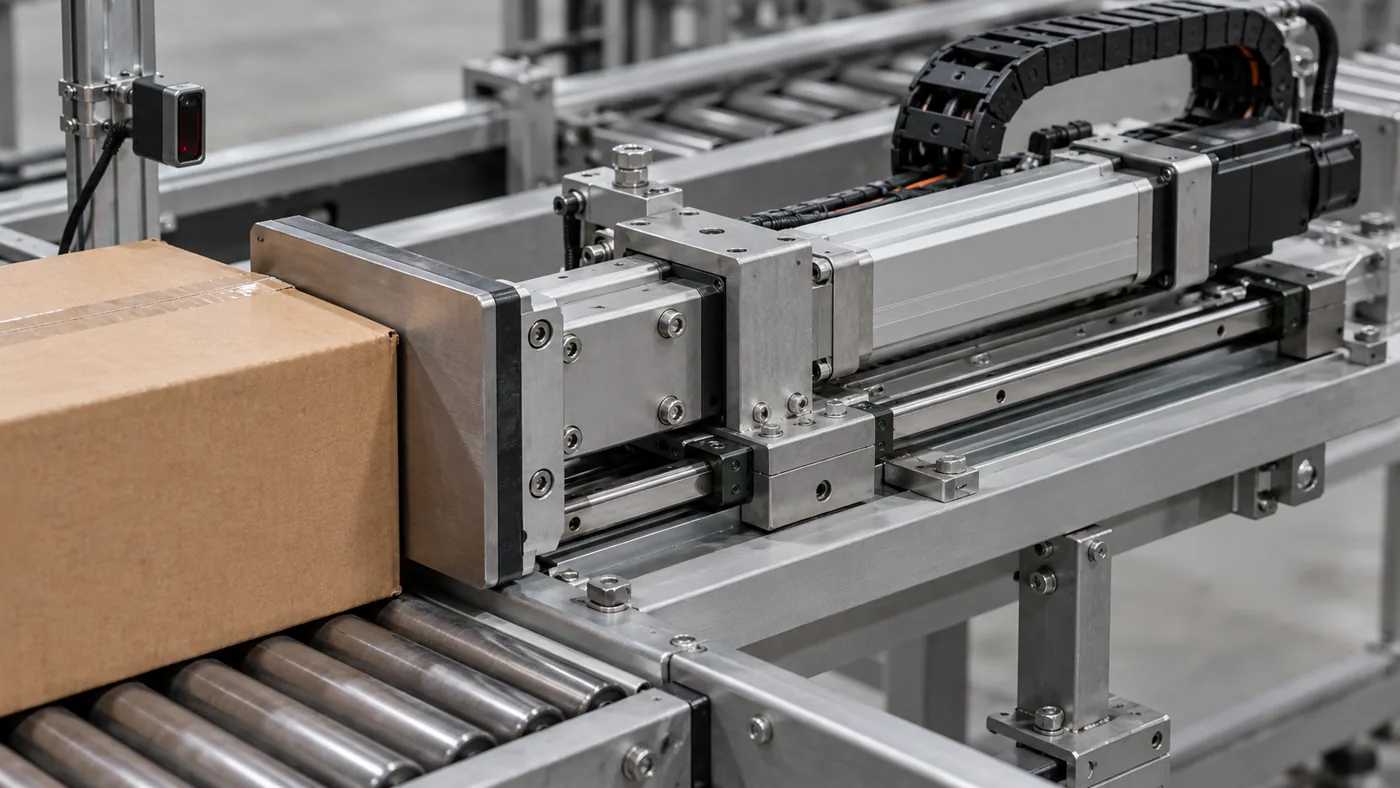
Guide the pusher and protect the product window.
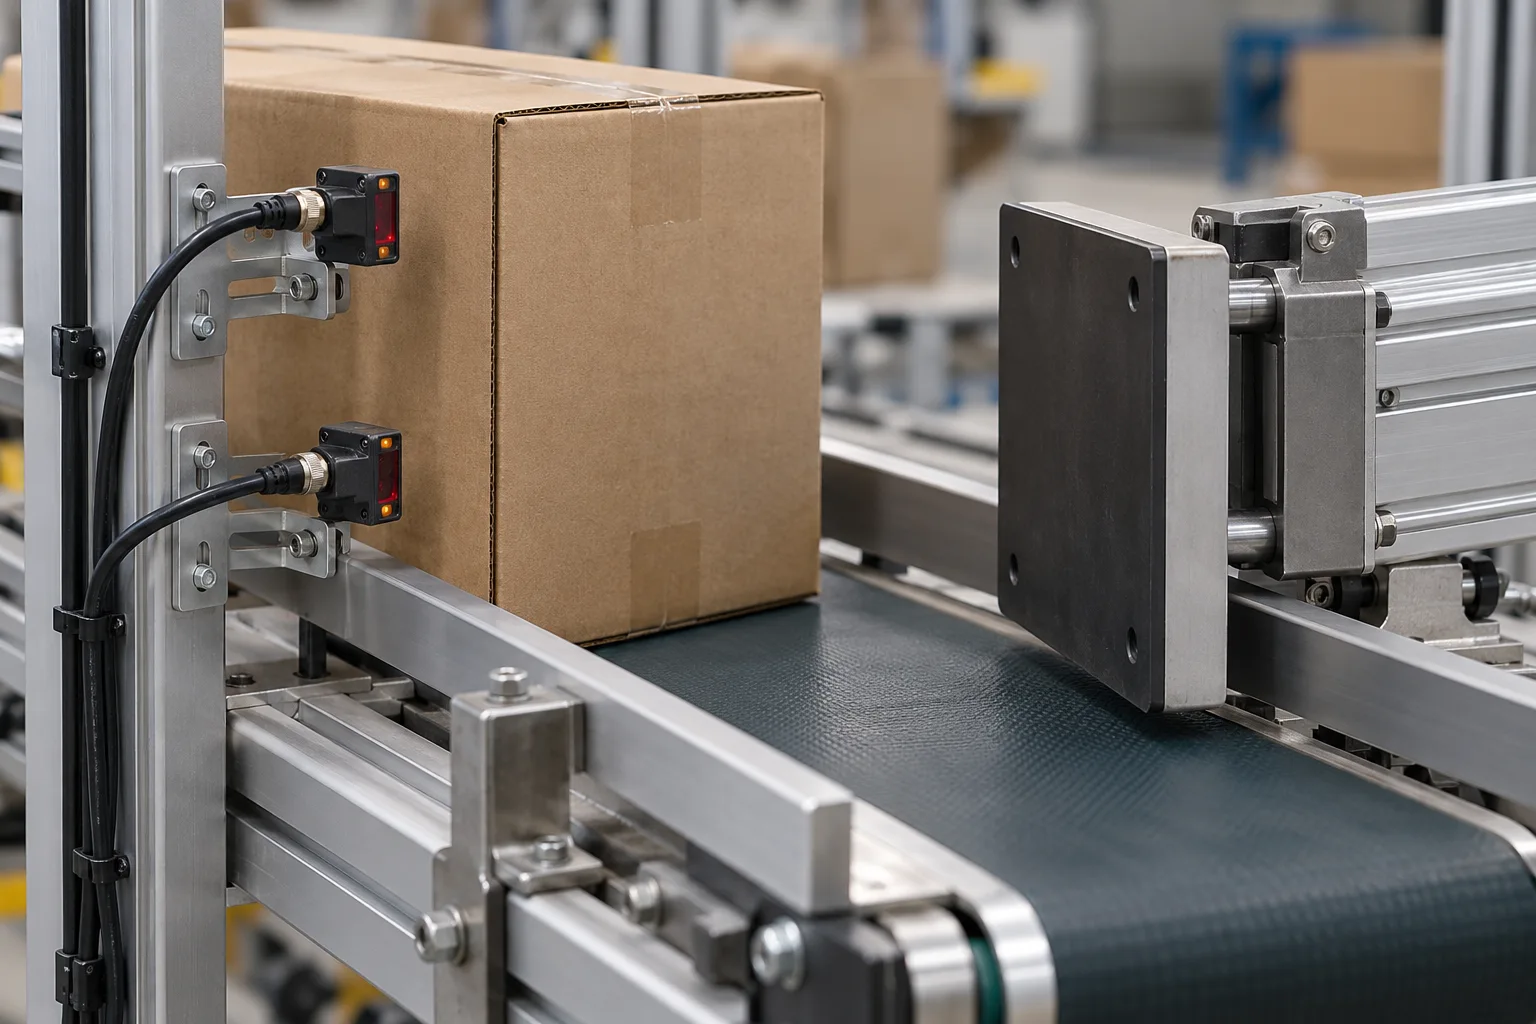
An externally guided pusher
The carriage carries offset moments, with clearance for skewed cartons. A broad contact face distributes the transfer force without loading the cylinder rod sideways.
A defined product window
Photoeyes confirm arrival and clearance. Relate sensing latency and conveyor speed to the available transfer window, with jam detection and a controlled reset.
Travel comes from the complete speed profile.
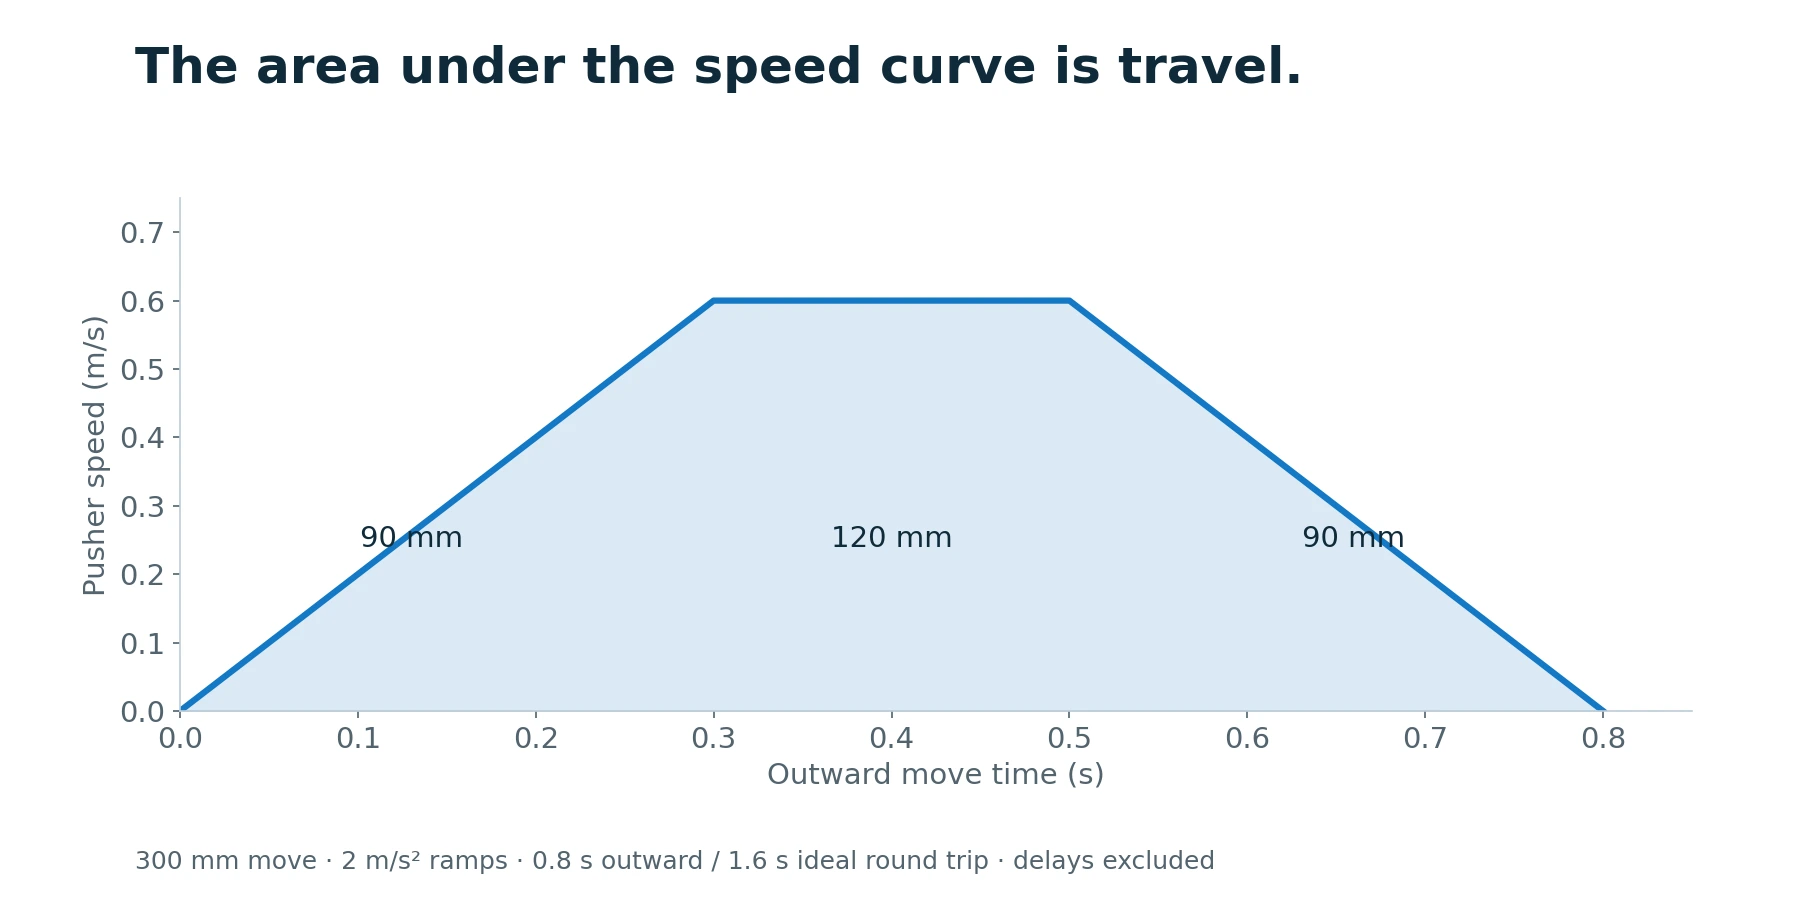
At 0.6 m/s and 2 m/s², each ramp takes 0.3 s and covers 90 mm. The remaining 120 mm takes 0.2 s: 0.8 s outward, or 1.6 s ideal round trip. Detection, dwell and conveyor delays add time. Size the total moving carriage and payload together.
A controlled cycle has defined exit conditions.
Detect and authorize
Identify a qualified carton and confirm lane availability, carriage reference and line-ready conditions.
Track arrival
Use the line timing/encoder architecture to predict the transfer window and reject stale triggers.
Transfer
Execute the product-specific profile while monitoring permitted load, travel and time.
Verify and return
Confirm the transfer and retract before the next approved window.
Handle a jam
Stop the defined sequence, identify carton state and perform controlled clearance; prevent an automatic second hit on an unknown carton.
Check before resetting: Late transfer: Check trigger position, conveyor-speed reference, communication delay and the complete occupied time. Carton rotates or tips: Review contact height/area, acceleration, lane support and carton variability.
Verify the product window and carton clearance.
Target
Proposed transfer trial: 100 consecutive cartons at the agreed conveyor/product window, with zero missed transfer commands or carton damage. The 1.6 s calculation excludes sensing, dwell and conveyor delays; production throughput must be measured.
Method and record
Measure product detection-to-motion latency and carton arrival window at minimum/nominal/maximum conveyor speed. Verify clearance with the largest carton and worst permitted skew. Record actual outward/return times and motor temperature. Challenge missing carton, blocked guide and late arrival with an approved recovery sequence.
Record actual value, conditions, uncertainty, result and approval. Test status: planned; measured results remain to be recorded at FAT.
Specify the actuator and its interfaces.
The useful RFQ includes line speed, carton spacing, product dimensions, receiving-lane geometry and the full transfer/return window. It should also state who owns tracking logic and product-damage acceptance. That information avoids selecting an axis from thrust and stroke alone.
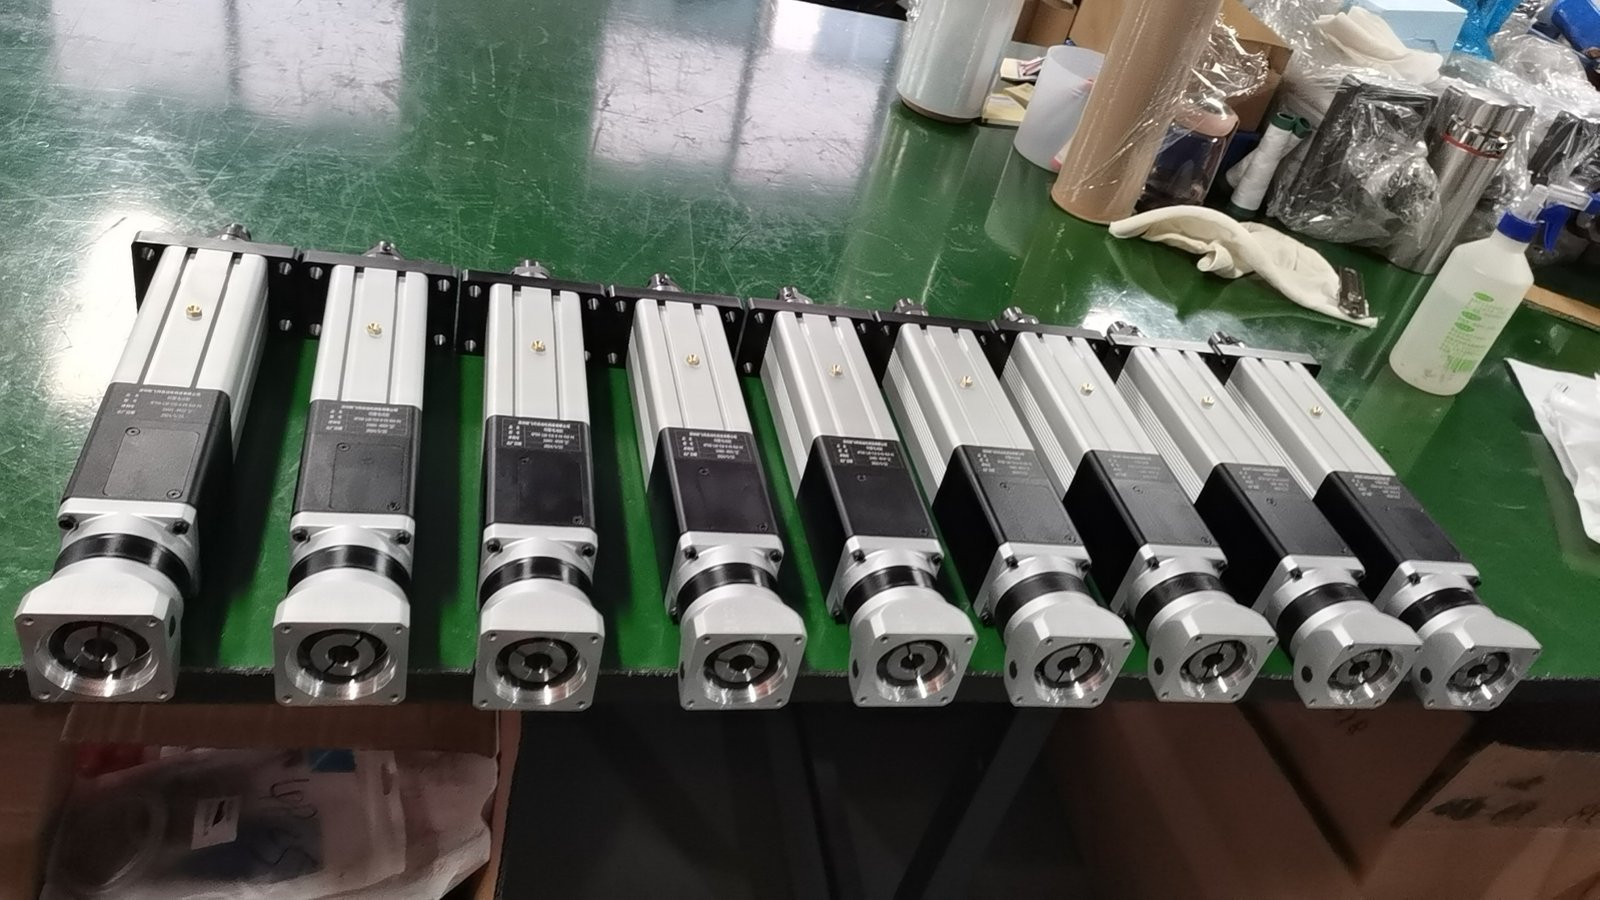
Confirm thrust versus speed, stroke, duty, mounting, motor/drive, feedback and environment together. The NFT40 photograph illustrates the product family; the study does not select that exact model.
Engineering pack: operating-cycle sizing, configuration and interface drawing, responsibility split, lubrication provisions and an agreed test plan.
Clarify the decision before quotation.
Acceleration, outbound and return stroke, dwell, sensing latency and product clearance all occupy the line window. The complete sequence must fit.
Only if the qualified size, mass, strength and timing envelope supports it. Different products often require bounded profiles and controlled recipe selection.
Request the configuration-specific sizing review, interface drawing, supply boundary and proposed acceptance plan. This feasibility study contains assumed inputs and calculated values; it does not report a delivered customer project or completed FAT.
Let’s engineer your next motion project.
Share the drawing, load cycle and acceptance target. Start with a clear actuator scope and the engineering checks that matter to your machine.
Drawing · Load cycle · Control requirements
Share
Drawing + operating cycle
Review
Loads, interfaces + duty
Confirm
Configuration + test plan
Deliver
Agreed hardware + records