Programmable pressing, locating and transfer motion for automotive assembly and EV production equipment.
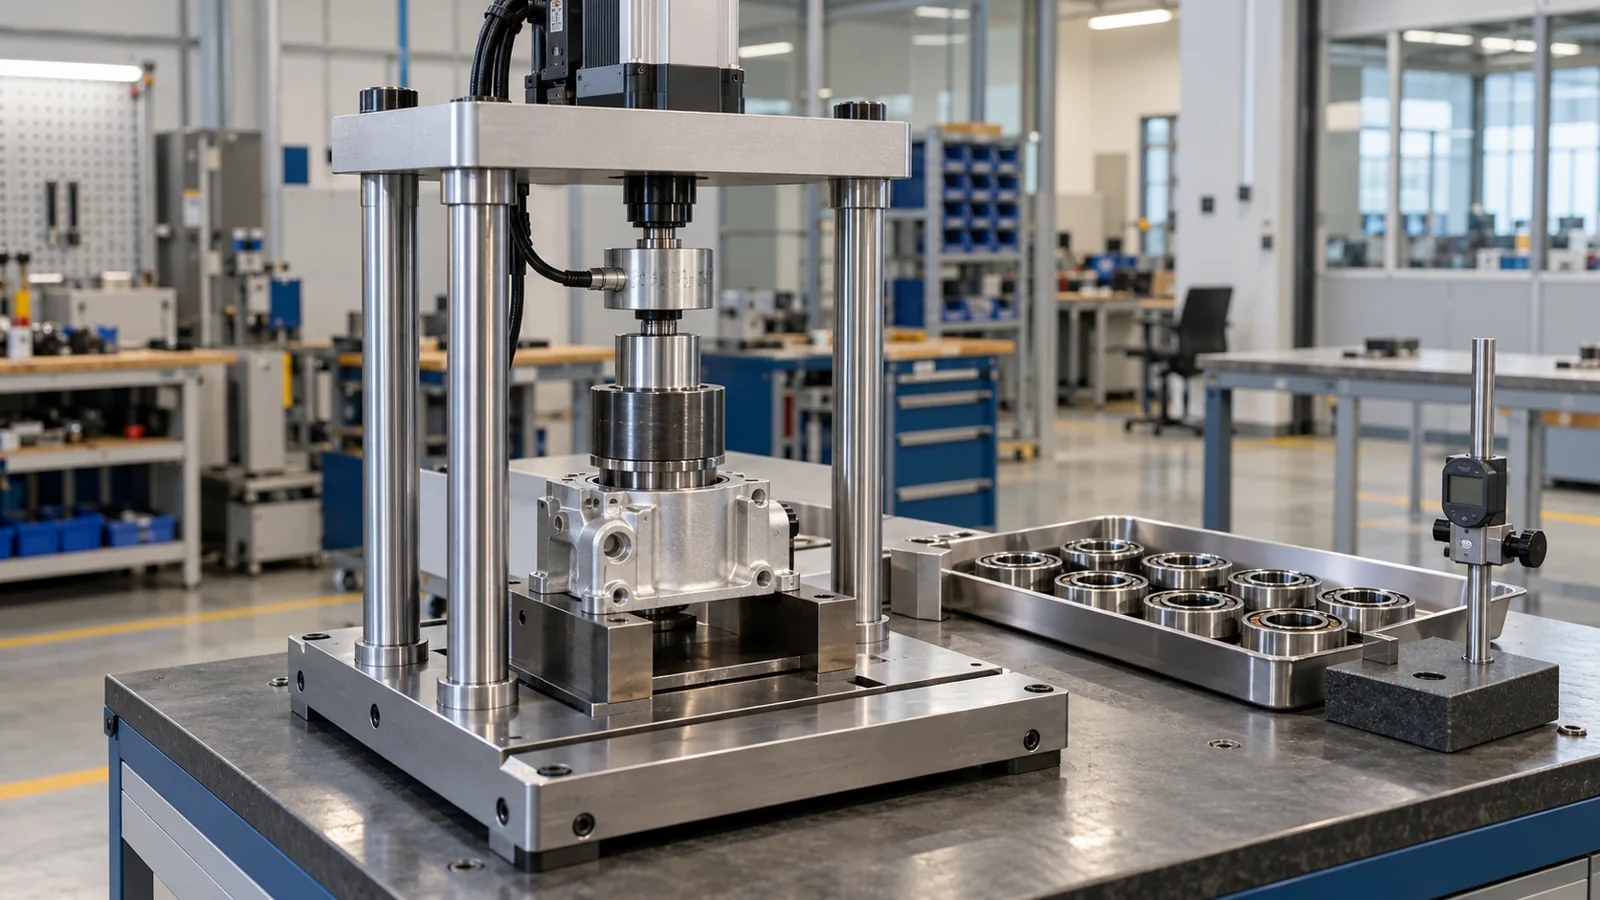
Use an approach, contact, pressing and return sequence with force versus displacement monitoring to identify assembly variation.
Apply controlled locating or clamping motion while reviewing insulation, tooling alignment and the process load profile.
Position clamps and fixtures to defined recipes; isolate tooling side loads through external guidance.
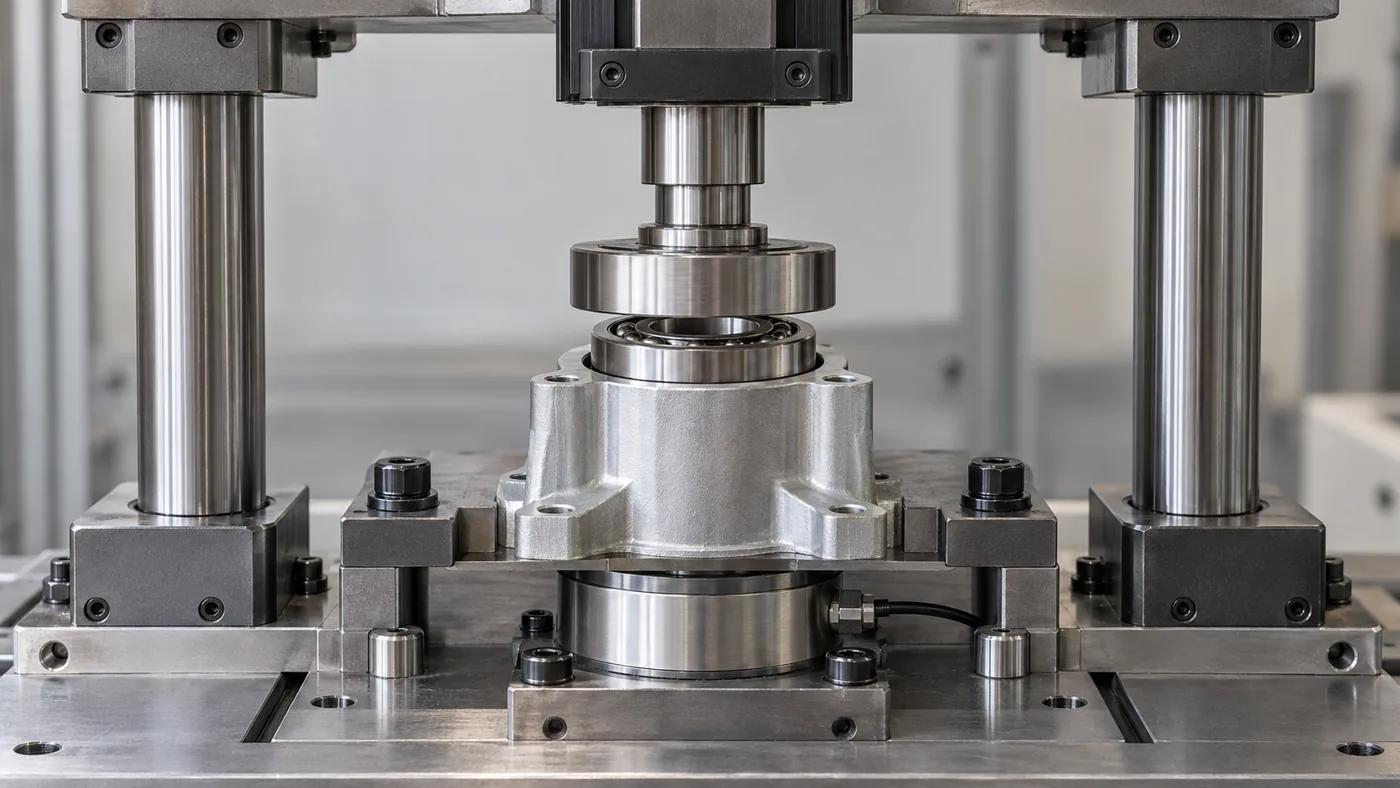
Programmable pressing, locating and transfer motion for automotive assembly and EV production equipment.
Review the operating challenge, proposed actuator arrangement, selection inputs and validation plan.
Insertion force curve, peak thrust, dwell and overload limit
Tool approach, part insertion depth, retraction clearance and reserve travel
Approach, contact search, pressing and return profiles
Encoder plus calibrated load cell when process force acceptance is required
Frame stiffness, parallelism, platen guides and tooling datum
Part presence, guarded cycle permission, curve logging and reject handling
Share the drawing, load cycle and acceptance target. Start with a clear actuator scope and the engineering checks that matter to your machine.
Drawing · Load cycle · Control requirements
Drawing + operating cycle
Loads, interfaces + duty
Configuration + test plan
Agreed hardware + records